From Laboratory Fermentation to Commercial Production

InnoTech Alberta’s Fermentation Plant is one of the largest publicly owned fermentation facilities in North America, with nearly 40 years of continuous operation supporting clients across industrial biotechnology, agriculture, food and feed ingredients, specialty chemicals, and bio-based products.

The facility provides the infrastructure, regulatory recognition, and technical expertise needed to develop, optimize, and scale biological processes from laboratory development through pilot-scale validation, demonstration production, and commercial manufacturing. 

Organizations use the facility to reduce scale-up risk, generate material for regulatory and market-development activities, support technology transfer, and accelerate commercialization of fermentation-based products.

To learn more about how we can support your project, visit our Fermentation Services page or download our Fermentation Services Brochure.
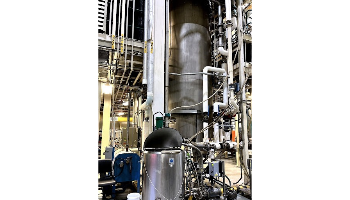
fermentation-plant

What's on this page?

What This Facility Enables

What This Facility Enables

Regulatory Recognition

Regulatory Recognition

Fermentation Infrastructure

Fermentation Infrastructure

Downstream Processing

Downstream Processing

Analytical Capabilities

Analytical Capabilities

Process Control & Data Infrastructure

Process Control & Data Infrastructure

Typical Applications

Typical Applications

What This Facility Enables

Organizations use our Fermentation Plant to:

  • Scale fermentation processes from laboratory to pilot and demonstration scale
  • Produce material for customer trials, field evaluations, and market development
  • Support regulatory submissions and certification activities
  • Generate data for technology transfer and commercial manufacturing
  • Optimize fermentation and downstream processing operations
  • Reduce commercialization risk before investing in dedicated production infrastructure
  • Manufacture products through contract and toll production arrangements

For many organizations, the facility provides an intermediate step between laboratory research and commercial production, helping de-risk technical and investment decisions.

Regulatory Recognition

Supporting Commercialization & Market Access

Regulatory requirements are often a critical component of technology commercialization.

Our facility maintains several regulatory recognitions that help clients generate product and supporting data for registration, certification, export, and market-entry activities. These recognitions are not tied to specific vessel sizes or production volumes and can support projects across multiple stages of commercialization.

USFDA: Registered facility for animal feed manufacture (registration applies below a defined annual supply threshold; contact us to confirm applicability to your project)

CFIA: Approved for animal feed manufacture for export to the EU

EPA: Registered facility for biopesticide production

EcoCert: Annually audited facility supporting client organic certification claims

Fermentation Infrastructure

Flexible Scale-Up Across Multiple Vessel Sizes

The facility operates 11 bioreactors across 6 vessel scales, ranging from 20 L to 15,000 L total volume. This multi-scale platform allows clients to evaluate how processes behave as production volumes increase while generating the operational data required for scale-up, optimization, and technology transfer.

All vessels are constructed of 316 L stainless steel and include:

  • Automated pH control
  • Backpressure control
  • Foam control
  • CIP capability
  • SIP capability
  • Off-gas analysis by mass spectrometry
  • Real-time process monitoring and data acquisition

Process data is continuously logged and trended using PI System historian software.

Station

Total Volume

Max Working Volume

Min Working Volume

8016, 8017

20 L

17 L

10 L

8035, 8036

150 L

110 L

60 L

8022, 8023

150 L

110 L

60 L

8050

450 L

350 L

250 L

8024

1,500 L

1,150 L

650 L

8030, 8031

7,500 L

5,500 L

3,500 L

8034

15,000 L

11,500 L

6,500 L


Key Operating Parameters

  • Aeration up to 1.5 vvm (vessel dependent)
  • Agitation up to 400 cm/s impeller tip speed (vessel dependent)
  • Temperature range: 6°C to 150°C
  • Positive-pressure operation
  • Oxygen enrichment available on select vessels
  • BSL-1 containment

Downstream Processing

Moving from Fermentation Broth to Finished Product

Commercialization requires more than successful fermentation. Our integrated downstream processing infrastructure allows clients to move from fermentation through recovery, purification, concentration, and finishing within a single facility.

Separation & Clarification

  • Disc-stack centrifuge (up to 10,000 L/hr)
  • Tubular bowl centrifuge
  • Microfiltration membrane modules
  • Ultrafiltration membrane modules (TFF)

Cell Disruption

  • High-pressure homogenizer
  • Dynomill (5 L)

Concentration & Drying

  • Vacuum and falling-film evaporation
  • Spray dryer
  • Lyophilizers

Solvent Extraction

  • Liquid-liquid extraction
  • Zone 2 classified, solvent-segregated workspace
  • Capacity for up to 2,000 L of flammable solvents including methanol, ethanol, and acetone

Analytical Capabilities

Data-Driven Process Development

On-site analytical support is available throughout process development, optimization, and production activities.

Capabilities include:

  • HPLC with UV, refractive index (RI), and fluorescence (FL) detection
  • Off-gas analysis by mass spectrometry
  • Phase-contrast microscopy
  • Colony-forming unit (CFU) enumeration
  • Real-time process data via PI System historian

These capabilities help clients understand process behaviour, improve productivity, troubleshoot performance challenges, and support technology transfer activities.

Process Control & Data Infrastructure

Advanced Process Analytics

A major differentiator of the Fermentation Plant is its integrated process monitoring and analytics platform.

All vessels are connected to automated monitoring and control systems that continuously track key operating parameters. Data is captured through PI System historian software, providing real-time acquisition, trending, analysis, and long-term archiving.

This infrastructure supports:

  • Process optimization
  • Scale-up studies
  • Batch documentation
  • Technology transfer
  • Regulatory documentation
  • Commercial deployment planning

The combination of real-time process data and vessel-wide mass-spectrometry-based off-gas analysis provides clients with detailed insight into fermentation performance across all scales.

Typical Applications

The facility regularly supports projects involving:

  • Industrial biotechnology
  • Agricultural biological products
  • Animal health and feed ingredients
  • Biofertilizers and biostimulants
  • Specialty chemicals
  • Bio-based materials
  • Environmental biotechnology
  • Microbial manufacturing platforms
  • Contract manufacturing and toll processing

For more information

Fermentation Plant

250 Karl Clark Rd NW
Edmonton, AB
T6N 1E4